This guide explains Pmoc Abrava in an objective, industry-focused way, outlining what it is, why it matters, and how to evaluate sourcing and handling. We then discuss practical selection criteria—such as supplier capability and documentation—followed by a comparison table, a step-by-step checklist, and conditions/requirements. Finally, FAQs address common compliance and quality concerns.
Pmoc Abrava is commonly discussed in professional procurement and technical communities as a specialty chemical designation tied to process performance, handling requirements, and documentation expectations. In practice, stakeholders typically focus less on marketing claims and more on verifiable details: material characterization, traceability, compatibility with existing workflows, and the supplier’s ability to provide consistent specifications and quality records. For buyers, the safest path is to treat “Pmoc Abrava” as a procurement category that must be validated through evidence, not assumption—especially when intended for controlled manufacturing steps or regulated environments.
Because “Pmoc Abrava” functions like a procurement label, not a universal guarantee of composition, the true question for a buyer becomes: what exactly is being supplied and how reliably will it behave in my process over time? The answer is largely determined by supplier practices, including how the product is manufactured, how it is qualified, how changes are controlled, and how information is packaged and delivered to customers.
“Pmoc Abrava” appears as a term used to reference a specific substance or product identity used in industrial or laboratory workflows. However, the key practical point is that a label alone does not guarantee performance. In industrial settings, the purchasing decision should hinge on objective indicators such as:
From an industry expert perspective, these items form the backbone of a defensible procurement file—useful for internal audits, customer qualification, and troubleshooting when process outcomes deviate from expectations.
In many procurement systems, especially those feeding into regulated manufacturing workflows (pharma, medical devices, advanced materials, certain chemical intermediates), the buyer is expected to demonstrate that raw material sourcing decisions were based on risk and evidence. “Pmoc Abrava” therefore typically needs to be treated as a controlled supply with defined acceptance criteria, not merely a commodity purchase.
Buyers often ask, “How do I know I’m getting the right grade?” The very reliable answers come from a structured validation approach. For Pmoc Abrava, consider the following evidence-based checks:
Ensure the supplier can specify the intended identity unambiguously (chemical name, internal product code, CAS number if applicable, and any relevant synonyms). Then confirm the delivered material aligns with the stated specification—particularly any targets that influence downstream steps.
Identity confirmation can involve different layers, depending on the nature of Pmoc Abrava and your process: some materials require only a document match (name/code/purity statement), while others require more robust verification such as spectroscopic confirmation (e.g., NMR/IR) or orthogonal analytics (e.g., HPLC with specified methods). Even if the supplier provides high-quality test results, buyers should ensure that the test methods and acceptance criteria are meaningful for their intended use.
A strong supplier will provide batch-level documentation that enables traceability. This is crucial when you need to investigate variations in yield, impurities, or stability.
Traceability is not just about receiving a batch number; it is about connecting that number to a complete set of manufacturing and testing information in a way that your organization can preserve and reference later. For example, if a deviation is detected in a downstream step, you may need to link the issue to specific incoming lots and to the specific upstream controls that were used when producing those lots.
In practice, many companies include in their qualification file: the supplier batch record summary (or equivalent), the certificate of analysis (CoA), any stability/shelf-life statements, and the shipping/handling details that show the material was received within the acceptable temperature or humidity window. The supplier’s ability to provide that package consistently matters more than the presence of any single document.
Even when the material is “correct,” compatibility issues can arise: moisture sensitivity, temperature constraints, incompatible containers, or solvent interactions. For Pmoc Abrava, the supplier’s handling guidance should be reviewed and mirrored in your SOPs.
Buyers sometimes underestimate handling requirements by treating them as generic EHS information. But specialty chemicals can exhibit performance shifts due to exposure to ambient conditions, headspace effects, absorption of moisture, or contamination from improper closures. If the supplier indicates a specific container type, inert atmosphere requirement, or recommended pre-drying, these details should be operationalized. Your SOPs should align with the supplier guidance so that the material performs as expected once it reaches the process.
Compatibility extends beyond the chemical itself. It includes compatibility with your equipment and workflow: transfer lines, filtration media, reactor materials, metering systems, and even cleaning agents. For instance, if Pmoc Abrava is sensitive to residues or has compatibility constraints with certain seals or gaskets, a mismatch can introduce performance issues that have nothing to do with supplier quality—but everything to do with the buyer’s integration of the material into the plant.
Where feasible, perform incoming inspection aligned with your risk profile. Many companies use a combination of documentation review and selective lab testing, tailored to the criticality of the step where Pmoc Abrava is used.
Risk-based incoming inspection can be structured as: document-only release for low-risk applications, document plus non-destructive checks (e.g., appearance, packaging integrity), and document plus analytical verification for high-impact uses. The “high-impact” category is usually defined by whether the material affects potency, critical quality attributes, yield, or the likelihood of forming impurities that are difficult to remove.
If incoming inspection results diverge from supplier documentation, you may need to decide whether the discrepancy is due to analytical method differences, sample handling, or a genuine out-of-spec condition. A competent supplier relationship will support timely investigations rather than blame shifts.
Because price information can vary widely based on grade, volume, packaging, and documentation scope, the very defensible way to evaluate cost is to compare total procurement value. Rather than focusing solely on unit cost, include:
In professional purchasing, this approach helps you avoid hidden costs that can outweigh a lower sticker price—such as delays, rework, or batch rejections.
To make “total value” measurable, many procurement teams calculate not only the direct cost of goods, but also the downstream operational impacts: expedited shipping premiums, time spent on qualification/analytical testing, potential hold times in receiving quarantine, and costs of deviation investigations. In heavily regulated workflows, costs can escalate when batch release requires additional documentation or re-testing because the supplier’s CoA package is incomplete.
Another price trap is the assumption that higher unit price always correlates with higher quality. In reality, quality is defined by specification and controlled variability, not by brand prestige. A lower unit price supplier might meet your specification perfectly but requires extra incoming verification. Conversely, a higher unit price supplier might provide robust documentation but use packaging or handling practices that create risk in your environment. The best commercial evaluation accounts for your actual operational model.
The supplier details you choose can determine whether Pmoc Abrava is easy to qualify or difficult to justify during audits. Industry top practice emphasizes supplier capability and transparency. Consider asking for:
These elements enable you to keep procurement decisions defensible—even if internal stakeholders change or processes evolve.
Supplier due diligence can be formal (audits, questionnaires, site assessments) or practical (requesting relevant documents and evaluating consistency over multiple lots). For many specialty chemicals, the strongest predictor of smooth procurement is how the supplier behaves when you have questions: do they respond quickly, provide complete documentation for the specific lot, and support root cause analysis if a discrepancy arises?
In a qualification file, it is helpful to capture not only what the supplier claims but how they demonstrate it through delivered evidence. For instance, if you request a full CoA package and receive it promptly with method details, you gain confidence. If you receive partial results or unclear method references, it increases the burden on your internal QC and slows release timelines.
Additionally, buyers should consider whether the supplier uses robust change management. For example, if the supplier changes manufacturing equipment, refining steps, or impurity control strategies, they should notify customers or provide updated documentation. Without a change control process, a buyer might inadvertently use material that differs in meaningful ways while still being labeled under the same product name. That scenario is a common root cause of batch-to-batch inconsistencies.
When a buyer’s sourcing strategy is described as “nearby,” the practical goal is usually faster logistics, smoother coordination, and easier document exchanges. For many teams, this also means planning around local operational realities such as warehouse workflow, receiving hours, and internal documentation review cycles.
While exact delivery timeframes depend on carrier, hazmat classification, and inventory availability, “nearby” sourcing often improves your ability to respond quickly to batch questions—because communication and resupply can be coordinated with fewer handoffs.
From a quality perspective, shorter logistics chains can reduce uncertainty around storage conditions during transport. Even if the supplier provides correct handling instructions, real-world variables like loading time, warehouse temperature swings, or delays during customs clearance can affect certain moisture-sensitive or temperature-sensitive materials. Proximity does not guarantee correct conditions, but it can improve predictability and reduce the window during which conditions might drift outside acceptable limits.
Another often overlooked point is language and documentation clarity. In “nearby” sourcing, you may have greater consistency in the formatting of SDS documents, CoAs, and shipping records. That can reduce administrative errors and speed up receiving release. While this seems operational rather than chemical, documentation accuracy is a cornerstone of audit readiness.
| Evaluation point | Supplier approach aligned with industrial top practice | Risk if documentation is thin |
|---|---|---|
| Product identity clarity | Unambiguous naming, product code mapping, and consistent labeling | Misidentification during qualification and rework later |
| Batch traceability | Batch-level documents supporting traceability from shipment to records | Inability to correlate process outcomes with a specific batch |
| Analytical support | Objective test methods and results that match stated specifications | Uncertain quality, higher incoming inspection burden |
| Handling guidance | Storage/handling instructions that match the material’s hazard and behavior | Stability or compatibility issues that disrupt production |
| Change control | Clear communication if supplier processes or specs change | Unexpected variability and audit nonconformities |
| Procurement alignment | Pricing tied to grade, packaging, documentation scope, and reliable lead times | Hidden costs from delays, returns, or rejected batches |
Below is a practical, step-by-step approach used by many technical procurement teams when qualifying a specialty chemical material like Pmoc Abrava. This is written as a general guide; always follow your internal EHS procedures and the supplier’s official documentation.
Document exactly where Pmoc Abrava enters your process, how it is used (e.g., preparation steps, reaction conditions, or formulation role), and which outputs are sensitive to variation.
Criticality is often defined by the material’s proximity to a product’s final quality attributes. If Pmoc Abrava is used as a key intermediate in a reaction, small impurity changes may create disproportionate effects later. If it is used as a buffer or non-critical component, variability may have less impact. Regardless, defining criticality helps determine how strong incoming inspection needs to be.
Ask the supplier for a complete documentation package for the specific batch or lot you plan to order. Confirm that it includes the information you need to support qualification.
“Complete” means more than a single CoA. It may include: SDS, CoA with method references, batch identification details, packaging and storage guidance, and any relevant statements regarding impurities, stability, and recommended re-test or shelf-life periods. If your organization requires GxP-like documentation discipline, you may also request additional quality documents such as deviation summaries, certificate format standards, or statements of compliance.
Compare the supplier’s specifications to your process requirements. If you cannot locate a clear match (for example, if key impurity or purity targets are missing), request clarification before ordering larger quantities.
Specification fit should include an assessment of whether the supplier’s measured parameters align with what matters to your process. For example, your process might be sensitive to certain impurity classes that the supplier reports inconsistently or only reports as “total impurities” without specifying thresholds for specific contaminants. In such cases, the supplier can sometimes provide expanded reporting under a confidentiality or customer-qualification agreement.
On delivery, perform basic receiving checks: container integrity, labeling accuracy, and document completeness. If your process requires additional verification, schedule testing through your lab.
Receiving checks can be structured as a checklist that includes: verification of container seals, verification of lot/batch numbers matching documents, inspection for signs of leakage or moisture ingress, and confirmation that the packaging type corresponds to the supplier’s recommended container. For some materials, appearance changes may be an indicator of oxidation, contamination, or degradation. If your SOP includes such indicators, align them with supplier guidance.
For high-impact steps, run a controlled trial using appropriate safety and process controls. Track measurable indicators such as consistency of performance, stability over the required handling window, and any impurity-related flags your process monitors.
A controlled trial also serves as a practical integration test. It validates that your equipment, transfer procedures, drying/conditioning steps (if any), and measurement methods can handle the material correctly. If you have a validated analytical method for performance verification, you can use it to compare results across trial lots. If you lack a direct performance test, you can use surrogate indicators such as impurity profiles, reaction rate consistency, or yield distribution patterns.
Maintain an internal record that includes: supplier documents received, results from any incoming checks, trial outcomes, storage/handling observations, and approval or conditional approval decisions.
A good qualification record is not just a folder of PDFs. It typically includes a rationale: why the supplier’s specifications were considered acceptable, what acceptance criteria were used for incoming release, and how deviations (if any) were handled. If the qualification is conditional, the record should define exactly what must be proven in the next batch or what additional monitoring will be required.
Once qualified, define how you will handle future batches: review cadence for certificates and test reports, escalation thresholds, and a change notification process aligned with your supplier relationship.
Ongoing supply practices can include: periodic review of CoA consistency, trend analysis of key parameters, and a defined response plan when results drift near acceptance limits. Many buyers implement “statistical awareness” even without fully formal SPC—if assay values or impurity patterns trend unexpectedly, they increase sampling or require investigation.
To support a robust procurement outcome, many organizations apply the following conditions/requirements when working with a specialty category such as Pmoc Abrava:
Qualification defensibility also hinges on discipline in routine operations. If a buyer receives materials but stores them incorrectly, uses unauthorized containers, or fails to record batch numbers consistently, then even a qualified supplier cannot guarantee performance. Auditors typically look for consistency: the same process that was validated during qualification should remain implemented.
Another key requirement is management of deviations and nonconformances. If a delivered batch fails acceptance criteria, the organization should have a clear decision tree: quarantine, evaluate the impact on production, consider whether deviation investigation is required, and determine whether the material can be released with exceptions or must be rejected.
In chemical sourcing, buyers increasingly emphasize documentation because it improves decision quality. For example, the International Organization for Standardization (ISO) frameworks widely influence supplier quality management systems. While the exact standard depends on industry and region, the underlying principle is consistent: measurable controls reduce variability and improve traceability.
For guidance on chemical safety information, the Globally Harmonized System of Classification and Labelling of Chemicals (GHS) is widely referenced internationally. Buyers typically expect SDS materials and labeling practices aligned with GHS concepts through local regulatory implementations.
Reliable references: ISO standards are maintained through ISO’s official publications; GHS is maintained via the UN framework for hazard communication (United Nations). These bodies support the broader expectation that chemical procurement should be underpinned by standardized information and risk communication.
Documentation and traceability matter because they provide the “audit trail” that ties the chemical’s origin to the chemical’s use. In complex manufacturing, problems are rarely attributable to a single factor. Traceability reduces time-to-root-cause by enabling targeted investigations rather than broad speculation.
In supplier relationships, documentation also provides a common language. When a buyer needs clarification about a parameter, a method, or an impurity limit, the supplier’s documentation becomes the basis for structured technical discussion. Without that shared documentation foundation, conversations become qualitative and difficult to resolve.
Pmoc Abrava is generally used as a product or designation term in procurement contexts. Because similar labels can be interpreted differently across suppliers, the safest approach is to confirm identity through the supplier’s official product documentation (including the specification and any relevant identifiers).
In other words, “what it is” should be treated as something you validate through documentation rather than something you assume based on name similarity. This is particularly relevant when multiple suppliers offer products that may be marketed under similar shorthand labels but differ in grade, impurity profile, or physical form.
Request a documentation package tied to the intended grade and batch, including specification details and analytical support. Then compare those details to your process requirements. If your use is sensitive, include incoming inspection or a controlled process trial before scaling.
In practical terms, confirm at least the three “anchors”: identity (name/code), specification (purity/assay and key impurity parameters), and evidence (test reports and method details). If your process is unusually sensitive, you may also require additional testing such as impurity screening, moisture content checks, or stability assessments aligned with your handling window.
“Nearby” typically affects logistics and communication speed more than intrinsic chemical properties. Quality still depends on supplier processes, batch consistency, storage conditions during transit, and the completeness of documentation. If logistics are tighter, receiving checks can also be performed more quickly, which can improve confidence.
Even though proximity cannot eliminate variability, it can reduce the time the material is exposed to uncertain transport conditions. It can also improve operational responsiveness if a discrepancy arises—allowing you to quarantine and clarify issues more quickly, which is itself a quality control measure.
Unit price matters, but total value matters more: packaging type, documentation scope, lead time reliability, and the supplier’s quality support. A lower unit price can be offset by delays or qualification issues if batch records and specifications are incomplete.
Additionally, consider whether the price includes any form of technical support or includes access to batch-specific documentation promptly. Some suppliers may offer lower pricing but require more back-and-forth to obtain the information needed for qualification. That “information friction” can carry hidden labor costs and can delay production timelines.
Require SDS access, storage guidance aligned with the material’s properties, and clear receiving/handling SOP requirements in your facility. Also ensure internal training and incident response procedures are in place.
Safe handling is not only a matter of PPE and SDS reading. It also includes: how material is transferred (to prevent contamination and exposure), how spills are managed, how waste is segregated, and how containers are labeled after opening. These steps influence both safety and quality performance. A material that is handled inconsistently may degrade, creating downstream variability even if the supplier product itself was within specification when received.
Maintain batch traceability, review batch documentation upon receipt, and define acceptance thresholds. When variability affects outcomes, escalate to the supplier with batch identifiers and request investigation through their change-control and deviation processes.
When variability emerges, consider analyzing it at two levels. First, confirm whether supplier-provided metrics (assay, impurities, physical characteristics where reported) also indicate differences. Second, verify that your handling and process inputs remained consistent across batches. This two-lens approach prevents blaming the supplier when the root cause is operational integration, and it prevents blaming operations when the root cause is upstream manufacturing change.
Yes, once qualification is achieved. Many organizations maintain approved supplier lists and require re-qualification when specifications change. The goal is consistency—so your internal process and audit documentation can rely on verified information.
However, supplier standardization should not prevent oversight. Even an approved supplier can experience changes in manufacturing sites, refining steps, analytical instruments, or impurity control strategies. Your change notification process should therefore include both “headline” updates (spec changes) and “subtle” updates (method changes, equipment changes) that can influence results even if final specs appear unchanged.
When buying Pmoc Abrava, the very effective strategy is evidence-led qualification: verify identity, request complete batch documentation, confirm handling requirements, and align supplier capability with your process criticality. By treating “Pmoc Abrava” as a procurement category that must be validated through objective materials and transparent supplier practices, you reduce risk, improve consistency, and strengthen audit readiness—without relying on assumptions or marketing language.
Ultimately, suppliers matter because chemicals are not static; they are produced under conditions and controlled by systems. Your procurement strategy should therefore be designed to “follow the evidence” from supplier identity to batch traceability to safe handling and process performance. When that evidence trail is strong, your organization can confidently scale production, troubleshoot issues faster, and maintain defensible quality records across time and across audits.
Striking the Perfect Balance: Navigating Premiums and Out-of-Pocket Expenses in Senior Insurance Plans

Explore the Tranquil Bliss of Idyllic Rural Retreats

How to Make Lasting Memories at Disneyland Attractions

4rkojvsx Technology: Industry Insights and Buying Guide

Affordable Phones and Plans for Seniors

Affordable Full Mouth Dental Implants Near You

Unlock the Top Kept Secrets to Finding Your Ideal Dentist for Flawless Dental Implant Results!

Discovering Springdale Estates

Unveiling RS Sul Telecom Services

A Guide to Londonderry Towers for Informed Buyers
This guide explains what to evaluate at Londonderry Towers, from location character and building design to practical due diligence steps. Background research covers how tower-style residences are assessed by buyers and property professionals, including usability, maintenance considerations, and supplier oversight. It provides an objective framework for comparing options without promotional claims or unverified figures.
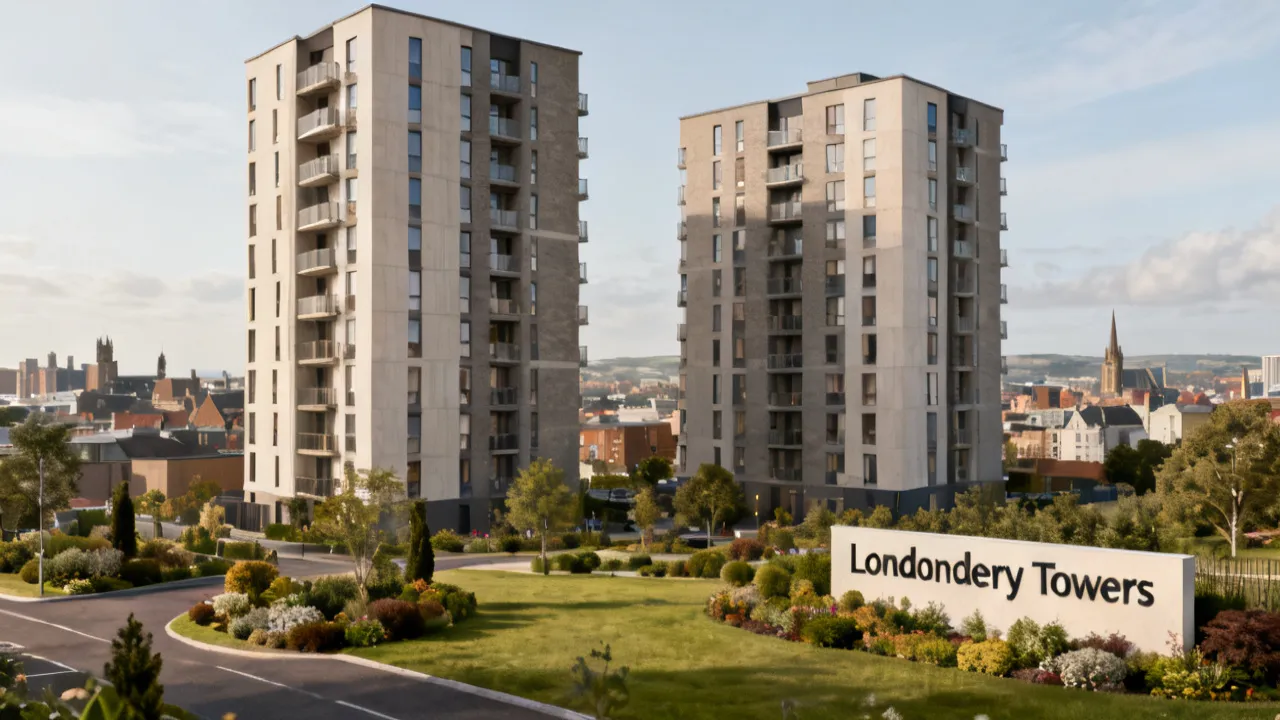
A Professional Guide to Londonderry Towers
This guide explains what to expect when evaluating Londonderry Towers, from location-led design choices to practical due-diligence steps for prospective tenants or buyers. It provides objective background on the role of residential towers in urban housing ecosystems, outlines how supply, amenities, and building operations affect day-to-day value, and frames key questions to ask before committing.
A Professional Guide to Londonderry Towers
This guide explains what to expect when evaluating Londonderry Towers, from location-led design choices to practical due-diligence steps for prospective tenants or buyers. It provides objective background on the role of residential towers in urban housing ecosystems, outlines how supply, amenities, and building operations affect day-to-day value, and frames key questions to ask before committing.
A Guide to Londonderry Towers for Informed Buyers
This guide explains what to evaluate at Londonderry Towers, from location character and building design to practical due diligence steps. Background research covers how tower-style residences are assessed by buyers and property professionals, including usability, maintenance considerations, and supplier oversight. It provides an objective framework for comparing options without promotional claims or unverified figures.
Pmoc Abrava: Industrial-Grade Overview and Use Cases
This guide explains Pmoc Abrava in an objective, industry-focused way, outlining what it is, why it matters, and how to evaluate sourcing and handling. We then discuss practical selection criteria—such as supplier capability and documentation—followed by a comparison table, a step-by-step checklist, and conditions/requirements. Finally, FAQs address common compliance and quality concerns.
